

Introduction — a question in the shop
Have you ever stood in a quiet mill room and wondered why a machine that looked perfect on paper still trips over simple jobs? In that hush I often think of CNC equipment manufacturers and the promises they make — and of the shop floor data that tells a different story (downtime, scrap rates, margin squeeze). Recent surveys show shops lose weeks a year to setup and misaligned toolpaths; the numbers are plain and painful. So what really separates a machine that sings from one that sputters? I want to walk you through that space—slowly, with a few hard facts and a sense for craft—before we compare options and move toward what to buy next.
Part 2 — Where common fixes fall short (technical breakdown)
Let’s be blunt and break this down: many shops look at cnc equipment for sale and buy to spec — spindle speed, advertised accuracy, a glossy control panel. But a spec sheet only tells part of the story. I see three repeat failures: misapplied toolpath strategies that ignore real-fixture errors, controllers that choke when you push complex G-code, and maintenance plans that treat servo motors and bearings like magic boxes. Each of these seems small until the part count tanks. Toolpath optimization, spindle speed matching, and the right feed rate matter more than raw horsepower. Look, it’s simpler than you think: if the machine can’t hold a micro-tolerance under thermal load, the neat spreadsheet specs won’t save your run. — and yes, I’ve watched shops replace whole machines when a control update would have fixed the issues.
Why do these fixes fail?
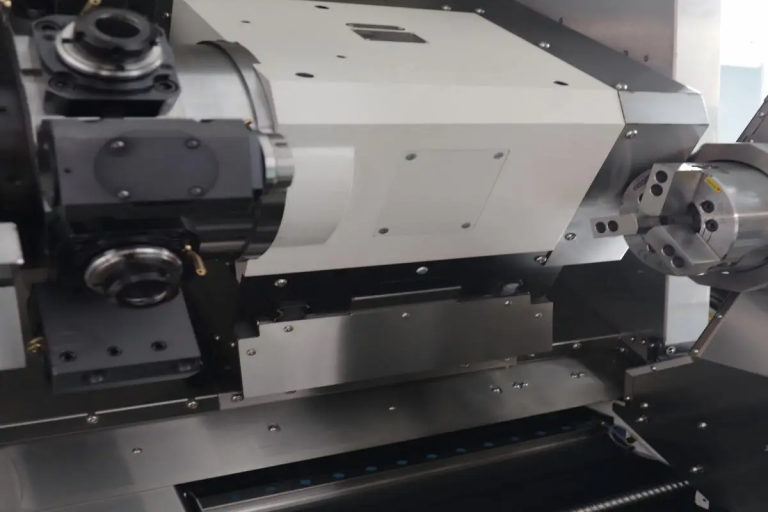
Technically, the root is mismatch: control logic, the mechanical envelope, and the operator’s workflow aren’t aligned. You can have excellent power converters and robust frames, but if the CNC lathe or mill is fed inconsistent tool offset data, the cycle still fails. I’ve altered toolpath strategies, tuned spindle speed curves, and updated backlash compensation in places where vendors insisted the defaults were fine. The result was less scrap, fewer touch-ups, and happier machinists. You don’t need mystery. You need systems that communicate — true real-time feedback, clear maintenance logs, better integration between sensor feedback and controller decisions. In short, stop treating machines as black boxes.
Part 3 — Looking ahead: small changes, big gains
Now let’s look forward. I like to think in two ways: one, the practical steps shops can adopt tomorrow; and two, the tech trends that will matter in five years. For the immediate future, tighter integration of controllers with edge computing nodes and smarter toolpath software gives a huge return. For example, a cnc milling company I worked with shifted to a predictive maintenance routine tied to vibration and spindle temperature sensors. Within months, unplanned downtime dropped and setup times shrank. This wasn’t magic — it was data fed back into the control loop and acted on.
What’s Next — real-world impact
I expect to see more shops use lightweight edge analytics to manage servo motors and spindle health in real time. Power converters and thermal models will be standard considerations during procurement, not afterthoughts. And yes, we’ll still tune G-code by hand sometimes, because human judgment matters with oddball parts — but we’ll do it with better data. — funny how that works, right? Here’s what I advise when you compare options: 1) check how well the machine’s control integrates with shop software, 2) verify real thermal stability at working RPMs, 3) insist on clear maintenance telemetry. Use those three metrics and you’ll cut the guesswork. I’ve seen the difference. For guidance and tools that feel built for real shops, see Leichman.