

Introduction: A Shop Floor Moment, Some Numbers, and the Question I Keep Asking
I was standing by the coolant sump when a young operator told me, “We can’t keep chasing setups like this” — and I felt that. Across small and mid-sized shops, downtime from complex setups eats up 20–35% of available spindle hours every month (no, that’s not a typo). In the same breath, 5 axis machining center manufacturers such as DMG Mori, Makino, Haas, Okuma, and Hurco keep promising faster cycles and smarter CAM integration — but are shops actually getting that promised uptime? I ask this because I’ve seen the tools on paper and the chaos on the floor. (It’s messy, and yes, I’ve tripped over a fixture plate more than once.) Let’s cut through marketing and look at what really helps a shop choose wisely — and how small changes can save hours, not minutes. Next: why the usual fixes still leave shops frustrated, and what that means for your throughput.
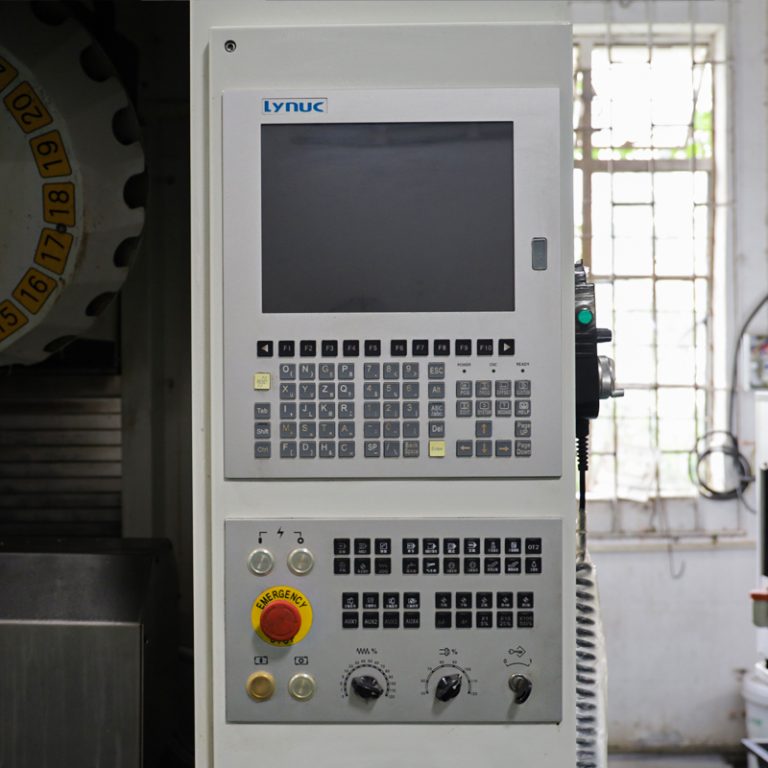
Why Traditional Fixes Fall Short for 5 axis high speed machining
5 axis high speed machining promised to be the cure for long cycle times, but the old tool-and-fixture playbook often misses the mark. I’ve watched shops add faster spindles and newer tool changers, then act surprised when chatter or poor surface finish shows up. The problem isn’t always the hardware — it’s the mismatch between tool paths, CAM post-processing, and machine dynamics. Spindle speed alone won’t fix a bad tool path optimization, and servo drives can only perform if the CAM understands the machine kinematics. Look, it’s simpler than you think: pushing RPMs without tightening the process is like speeding a car with worn tires.
Here’s the real flaw: vendors sell discrete upgrades (higher spindle, more tools) rather than workflow fixes. That leaves shops juggling manual offsets, clumsy fixtures, and unpredictable probe routines. I call out three specific gaps I see all the time: poor integration between CAM and CNC controller, over-reliance on high feed rates without compensating for tool deflection, and underestimating setup repeatability. Those are not abstract; they cost real hours and bite into margins. When you see chatter or unexpected rejects, don’t blame the machine first — check the whole tool path, the fixture repeatability, and your cutter engagement strategy. Why? Because most shops can recover 10–20% of lost time by tightening those links — funny how that works, right?
Why can’t a simple upgrade fix it?
I’ll be blunt: upgrades address symptoms, not workflow. You need aligned CAM post-processing, consistent fixturing, and predictable cutting forces to make high speed strategies pay off. That trio is where most shops falter.
New Principles That Will Shape High Speed Machining Center Performance
So what should you change? I like to think in principles, not products. First: synchronize the whole chain — CAM, controller, machine dynamics. Second: measure and control cutter engagement with better toolpath strategies and adaptive feeds. Third: bake repeatability into fixtures and probe cycles so each job starts from a known state. When I discuss these ideas with shop owners, we talk spindle speed and torque, but we always come back to toolpath and setup. Integrating edge diagnostics and feedback loops (yes, even simple torque monitoring) helps too — because data without action is just noise.
To be concrete: modern shops use model-based tool offsets, closed-loop spindle feedback, and smarter collision-avoidance in CAM to run true high speed machining. Equip a high speed machining center with these practices and you cut cycle time and scrap. I’ve seen cases where throughput improves by 15–30% after process tuning — not from a single part, but from a focused program that included fixture redesign, CAM updates, and operator training. That’s the sort of win that sticks. — and yes, it takes discipline, but it pays back fast.
What’s Next: Practical Steps and Metrics
Here are three compact metrics I use when evaluating options for my clients: 1) Net spindle utilization (actual cutting minutes vs available hours), 2) First-pass yield for complex 5-axis parts, and 3) Average setup time per job changeover. Use these to compare machines and vendors on equal footing. When a manufacturer talks about peak RPM or tool capacity, ask for real shop data tied to those three metrics. I trust numbers that reflect the shop floor, not the spec sheet.
In short: pick partners who help you tighten the whole chain — CAM, fixture, and machine — and who provide actionable diagnostics, not just glossy brochures. We’ve learned the hard way that a little process work beats a big hardware splurge more often than not. For practical machines and process support, I look to brands that back their gear with system-level thinking — like Leichman.